

Introduction
One afternoon I was watchin’ Joe down at the fab shop—he’s got oil on his hands and pride in his face—trying to coax an old mill into doin’ something it just weren’t built for. CNC machining center manufacturers get this; they see shops like Joe’s every day. Recent trade notes say many small shops (I’d say around 60% by rough count) still wrestle with legacy machines and long setup times—so I gotta ask: how do we stop wastin’ hours on avoidable fixes? (I reckon we can do better.)
I write this plain: I’ve spent years walkin’ plant floors and pokin’ at control panels. I know what G-code looks like when it’s been hacked to death and how servo motors cough when they’re mis-tuned. The scene’s familiar: parts late, techs tired, and management lookin’ for a smoke-free fix. This piece pulls that moment apart — we’ll look at where the old fixes fail, what users quietly hate, and where new choices make sense. Stick with me; we’ll head into the nuts and bolts next — and yes, I’ll keep it simple. — funny how that works, right?
Peeling Back the Pain: Why Old Fixes Don’t Cut It
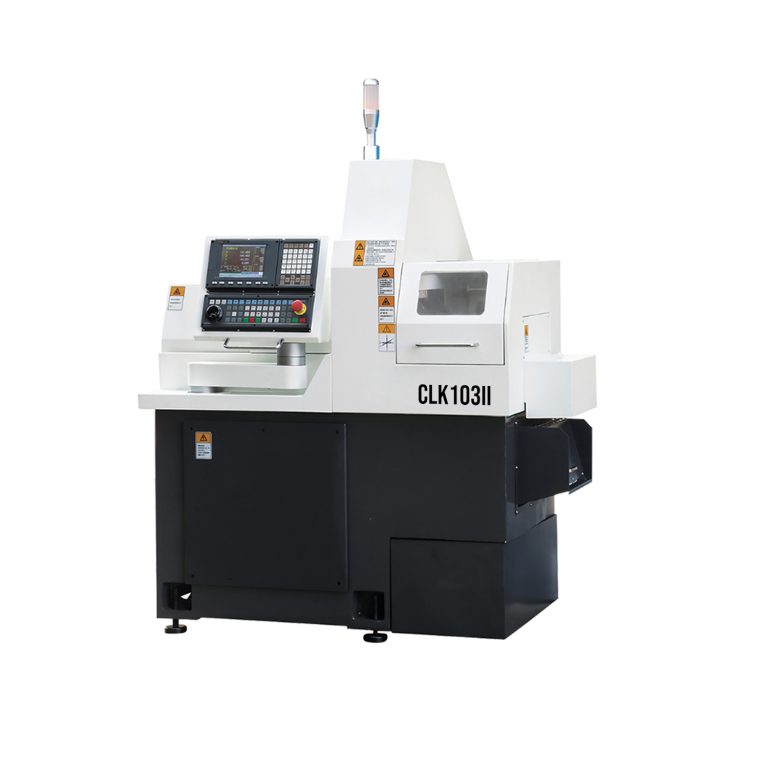
Let me be clear: when shops try to patch over problems, they often reach for band-aids that never held up. At the heart of the matter is the cnc turn mill center machine — a workhorse that folks expect to do more than it was ever set up for. Technically speaking, manufacturers gave us spindle speed ranges and heavy-duty tool changers, but the integration side — controls, workflow, and tooling strategy — is where things fall apart. Look, it’s simpler than you think: proper tool paths and rigid fixturing beat last-minute speed hacks every time.
What breaks first?
I see three common fractures. First, mismatch between CAM output and machine kinematics leads to chatter and scrap—ball screws and axis tuning are often blamed, rightly so. Second, the human factor: operators work around limits instead of fixing root causes, piling manual offsets and error-prone tweaks into the program. Third, upkeep is deferred; a worn spindle or a sloppy tool changer snowballs into downtime. We can name parts—spindle bearings, servo motors, feed drives—but the real cost is lost hours and faith. As I noted above, this isn’t just about parts; it’s about how we treat the machine as a system. If we keep bolting on quick fixes, the shop stays stuck.
The Road Ahead: Practical Paths and Real Gains
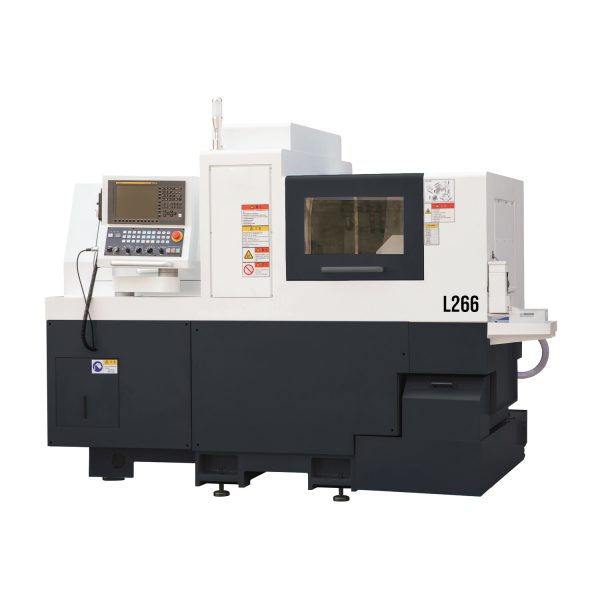
Now, let’s look forward. I want to talk about realistic choices—no vaporware. Newer systems combine better motion control with smarter CAD/CAM workflows and diagnostics that actually tell you what’s wrong. For shops thinking long-term, a step is to test a modern cnc center machine on a single high-mix cell. You get cleaner cycle times, fewer scrapped parts, and easier troubleshooting. And yes, there’s an upfront cost—power converters and upgraded I/O aren’t free—but the uptime gains show up quick.
What’s Next?
Here’s how I’d judge options. First, check how the machine handles tool paths in real setups (not in demo parts). Second, ask about diagnostics: can it flag a ball-screw wear trend or spindle vibration early? Third, consider integration: does the control play nice with your CAD/CAM and shop-tracking tools? Those three points guide me every time. Plus—funny how that works—teams are happier when the gear stops surprising them.
Practical Advice: Three Metrics to Choose By
I’ll leave you with three clear evaluation metrics I use when advising shops. One: mean time to setup — measure how long a real job takes from fixturing to first good part. Two: diagnostic transparency — can the machine log faults and suggest fixes, or do you get cryptic error codes? Three: total cost of ownership — not just sticker price but consumables, expected downtime, and training time. Use those, and you’ll stop buying boxes and start buying solutions. I say that because I’ve watched teams save weeks a year just by choosing better controls and clearer maintenance paths.
So if you’re pickin’ a partner for the next upgrade, weigh those metrics, test on real parts, and trust the crew who’ll run the machine day to day. We know the stakes: less waste, less late nights, better margins. For manufacturers and buyers ready to make a smart move, check what Leichman offers and think about fit, not flash. Leichman