

Introduction
Why do a single, brief spark and a misplaced strike translate into months of investigation and potential liability? Consider a confined-space entry where trace solvents linger; statistics show that tool-related ignition accounts for a disproportionate share of industrial incidents (OSHA reports and incident logs corroborate this). In that precise risk landscape, a non sparking hammer is not merely a convenience—it is a compliance vector and an operational control. Pursuant to prevailing safety codes and site-specific permit-to-work conditions, the selection of strike tools implicates hazard assessment, material compatibility, and maintenance regimes. I want to be plain: we must treat tool choice as contract-level risk mitigation, not an afterthought. This piece will unpack the problem drivers, expose hidden user pain points, and then point toward better technical principles—so let us proceed to the core failures that persist.
Deeper Faults: Why Standard Tools Fail Practically and Legally
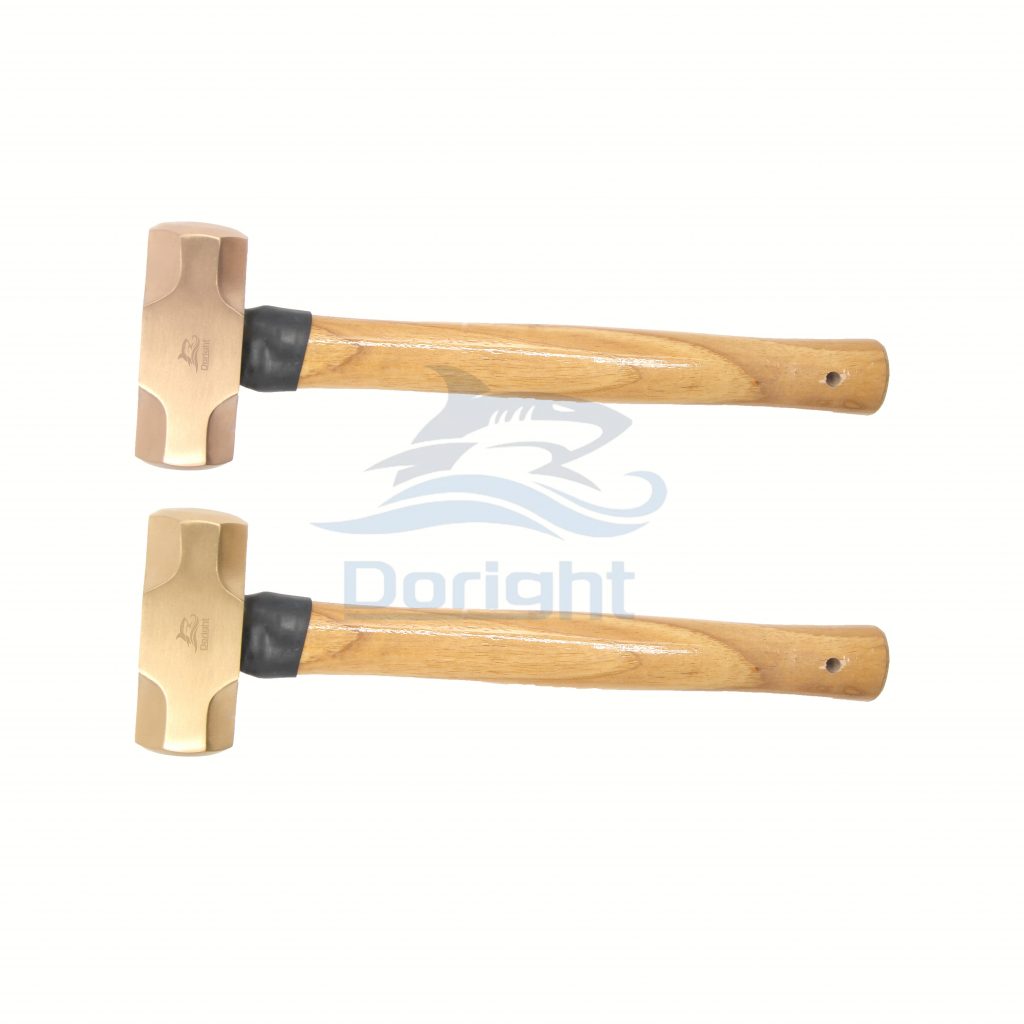
I start with the product that often gets misapplied: non spark hammer. In field audits I’ve conducted, the first 100 feet of a job site—the workshop, the rig floor—reveals repeated misuse. Technically, many crews treat non-sparking tools as a single-solution checkbox: if the hammer head is bronze alloy or beryllium copper, they think the job is done. But that reasoning fails when you account for wear patterns, surface contamination, and inadvertent contact with ignition-prone particulates. Terms to keep in mind: bronze alloy, spark suppression, hazardous atmospheres. The materials science works only when the tool’s life-cycle, cleaning, and joint integrity are managed; otherwise conductivity and micro-fractures produce the exact ignition mechanism we expect to prevent. Look, it’s simpler than you think—maintenance and training matter as much as material selection.
So what exactly is overlooked?
Two central flaws recur. First, procurement often prizes unit cost over lifecycle compliance: suppliers ship non-sparking materials that meet nominal specs but arrive with machining marks or improper tempering. That undermines spark suppression and can elevate frictional heating. Second, procedural drift happens: tools leave the hazardous zone without lockout/tagout verification; they accumulate ferrous contamination; their torque-readings—if applicable—are never recorded. These are operational failures (not product failures alone). I’ve seen permits revoked because a single contaminated hammer negated an entire hot-work permit—funny how that works, right? We need to treat non-sparking tools as engineered controls subject to inspection protocols, not disposable commodities.
New Principles: Engineering Safer Strike Tools for Tomorrow
Moving forward, I propose we adopt three guiding technical principles that realign procurement, maintenance, and field practice. First: certify materials not only for non-sparking properties but for sustained performance—consider ASTM-grade bronze alloy testing for abrasion resistance. Second: integrate inspection checkpoints into the workflow—visual checks, conductivity scans, and clear contamination logs. Third: design for repairability so that a worn face is replaced, not discarded; that improves both safety and cost-efficiency. Throughout these steps, the functional objective is to ensure intrinsic safety, reduce the probability of ignition, and preserve site-wide compliance.
What’s Next for tools and teams?
We should also watch emerging support tech—portable conductivity testers and simple contamination sensors—that can be deployed at the tool crib. When paired with disciplined permit procedures, these become tangible controls, not theoretical ones. I recommend piloting a program with a verified non sparking safety hammer fleet, baseline incident metrics, and defined inspection intervals. — and yes, that matters. The point is to shift from reactive replacement to predictive upkeep.
Evaluative Close: Metrics and Practical Guidance
In closing, I’ll give three concise evaluation metrics you can use immediately when selecting or auditing non-sparking strike tools: (1) Material Integrity Index — frequency of surface defects per 100 tools, measured after delivery and quarterly; (2) Contamination Control Rate — percentage of tools that pass contamination screening before entering hazardous zones; (3) Lifecycle Cost per Safe Hour — total ownership cost divided by operational safe-hours until replacement. Use these metrics in procurement specifications and in toolbox talks. They are measurable, actionable, and they align legal exposure with operational control.
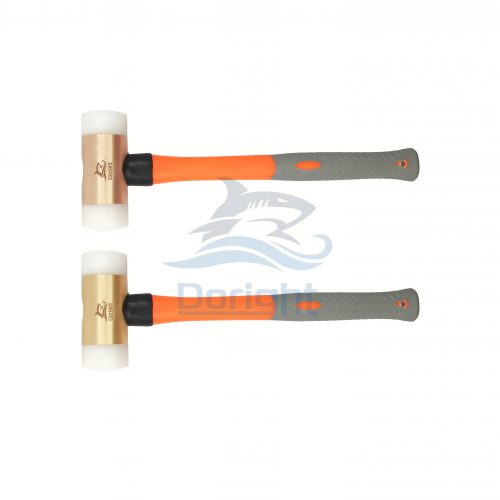
To sum up my view: choose tools that come with verifiable material data, attach inspection obligations to permits, and train crews to treat non-sparking hammers as engineered safety devices rather than incidental kit. I speak from audits and close calls—we can prevent avoidable incidents with clearer standards and modest procedural change. For vetted products and support, consult Doright.