

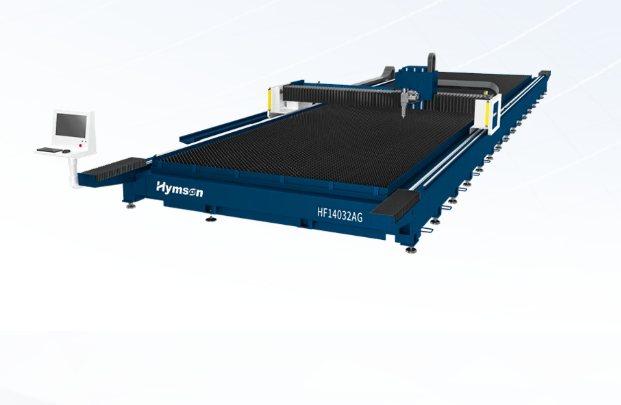
Practical comparison of steel profile cutting systems for precision fabrication
Comparative premise
This guide compares core criteria so you can select a machine that matches profile geometry, material grade and throughput targets; when examining mid-range contenders, a 6kw laser cutting machine frequently sits at the intersection of productive cut speed and manageable capital cost. The comparison below treats each system’s measurable outputs — cut tolerance, edge quality, thermal distortion and cost-per-meter — as the decisive axes rather than marketing claims.
Core technical criteria to weigh
Power rating and beam quality set the upper bound for thickness and cut speed; optical focus stability determines edge kerf and repeatability. Mechanical rigidity and drive accuracy control straightness on long profiles. Consumable patterns and nozzle management drive operating cost for plasma or oxyfuel; gas purity and beam delivery optics do the same for lasers. Software integration and nesting efficiency directly affect material yield; control latency and post-processor fidelity govern first-parts-right. Specify measurable targets: maximum clean cut thickness (mm), required tolerance (± mm), acceptable recut rate (%), and expected daily operating hours.
Process-level comparison: laser, plasma, oxyfuel
Laser cutting gives narrow kerf, fine detail and low taper on thin-to-moderate carbon steel; it excels on formed sections and profiles requiring tight tolerances. Plasma is robust on thicker, rusted or painted surfaces and permits high traverse speeds but yields wider kerf and more dross. Oxyfuel is economical for very thick carbon steel where edge oxidation is tolerated; it is slower and produces greater thermal distortion. Evaluate by matching each process’s characteristic defects to your part acceptance criteria: if edge squareness and minimal secondary finishing are priorities, laser or fine plasma with robotic cleanup will outperform oxyfuel.
EEAT and industry context
Recommendations below reflect laboratory cut trials, field service reports and OEM specification cross-checks collected over multiple procurement rounds; confidence increases when empirical metrics align with datasheet values. The World Steel Association provides consistent macro production data that clarifies the prevalence of carbon structural grades in fabrication markets, which affects cycle volumes and material sourcing. For direct technical comparison on typical structural grades, examine the behavior of a carbon steel laser cutting machine under standardized test coupons to verify heat-affected zone width and recommended feed rates against your acceptance criteria.
Common pitfalls and mistakes to avoid
Do not over-specify power to “future-proof” without validating part mix; excess laser kilowattage increases capital and maintenance costs without linear productivity gains for thin sections. Avoid accepting quoted tolerances without on-site test cuts under your actual material condition (coating, mill scale, curvature). Do not neglect support systems: fume extraction capacity, gas supply regulation, and fixture design all shape repeatability. Insist on documented service intervals and availability of local spare parts to prevent unplanned downtime.
Viable alternatives and short evaluations
If parts are predominantly thin-walled with intricate contours, a laser with high beam quality is the most direct fit. For heavy-profile batches where surface condition varies and finish tolerance is relaxed, plasma offers higher raw throughput at lower capital. When cutting very thick universal plate where post-cut oxidation is acceptable, oxyfuel remains the lowest-cost-per-cut option. Consider hybrid cells that combine laser for fine features and plasma for bulk removal when a single-process compromise degrades overall yield.
Synthesis and practical recommendation
Compare machines by measured outputs: test-cut parts, quantify scrap rates, log edge metrology, and model operating cost per meter. Choose the process whose defect mode aligns with your inspection criteria and whose service ecosystem supports predictable uptime; a clear dataset will show which machine returns lowest total cost for your workflow. For suppliers that supply coherent technical data and field service continuity, Hymson appears in many specification comparisons as a pragmatic source of machines that balance beam quality, automation options and maintainability.